 Get a quote
Resources
Key Drivers of Punching Machine Power Consumption & How to Reduce Them
TABLE OF CONTENTS 1. Core Machine Architecture Governing Electricity Draw • Drive Motor Capacity, Efficiency Ratings, and Powertrain Topology • Flywheel Inertia and Clutch-Brake Energy Losses • Hydraulic Pump Pressure and Flow Regulation • CNC Controller Intelligence and Motion Algorithms 2. Workpiece and Process Parameters Shaping Power Load • Sheet Gauge and Tensile Strength • Tooling Sharpness and Die Clearance Geometry • Ram Stroke Travel and Bottom-Dead-Center Dwell 3. Shop-Floor Operating Habits to Trim Kilowatt-Hours • Shifting Heavy-Tonnage Runs to Off-Peak Utility Windows • Streamlining Nesting and Tool-Path Sequences • Activating Standby and Automated Sleep Functions 4. Preventive Maintenance and Hardware Retrofits for Long-Term Savings • Deploying Condition-Based Predictive Maintenance • Installing Variable-Frequency Drives (VFDs) on Legacy Presses • Upgrading to Direct-Drive Servo-Electric Punching Systems 5. Frequently Asked Questions (FAQs) • Monitoring and benchmarking press power usage accurately • Accounting for compressed air consumption in auxiliary circuits • Evaluating the return on investment (ROI) of high-efficiency presses 6. Conclusion & JUGAO Energy Audit Support |
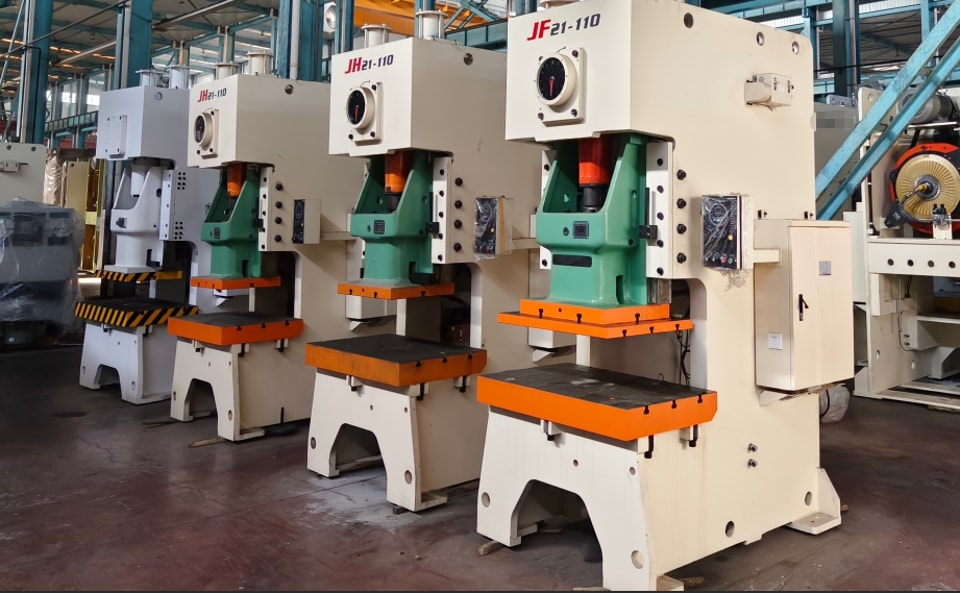
Evaluating presses on a busy fabrication floor quickly reveals that electrical draw is a silent overhead expense—often overlooked during daily production until monthly utility statements arrive. Understanding why two presses with comparable tonnage ratings exhibit dramatically different kilowatt-hour profiles is essential for protecting profit margins. In this technical guide, we examine the mechanical and operational factors behind punching machine energy demand, explain how to track power metrics effectively, and outline proven field methods to lower electricity consumption without compromising cycle speed or part precision.
1. Core Machine Architecture Governing Electricity Draw
Drive Motor Capacity, Efficiency Ratings, and Powertrain Topology
The primary drive motor accounts for the largest share of a press's electrical load. Modern direct-drive servo motors typically consume 10% to 25% less electricity than traditional hydraulic power units. Prioritizing motors certified to IE3 or IE4 efficiency standards—paired with regenerative drives that capture braking energy and feed it back into the DC bus—substantially reduces net power draw.
Flywheel Inertia and Clutch-Brake Energy Losses
Legacy mechanical punch presses depend on heavy rotating flywheels to accumulate kinetic energy, yet significant power is lost as friction and heat every time the clutch cycles. Contemporary pneumatic or hydraulic clutch-brake assemblies governed by smart logic minimize idle flywheel spin, curbing parasitic electricity waste between hits.
Hydraulic Pump Pressure and Flow Regulation
Conventional hydraulic punching presses keep fixed-displacement pumps running at peak system pressure continuously, even when the ram is stationary. Integrating variable-frequency drives (VFDs) or closed-loop servo-hydraulics synchronizes pump output with instantaneous forming demand, sharply lowering motor amperage during partial-load or standby intervals.
CNC Controller Intelligence and Motion Algorithms
Advanced CNC controls that calculate shortest-path tool routing, eliminate redundant air hits, and cluster adjacent perforations reduce both table travel time and total watt-hours per finished blank. Regularly updating controller firmware is an effortless optimization, as newer software releases frequently introduce refined acceleration profiles and power-management routines.
2. Workpiece and Process Parameters Shaping Power Load
Sheet Gauge and Tensile Strength
Shearing thicker plates or high-yield alloys such as stainless steel demands higher punching force, which translates directly into elevated motor current. Calculating required shearing tonnage per sheet prior to job quoting ensures accurate energy cost estimation before production begins.
Tooling Sharpness and Die Clearance Geometry
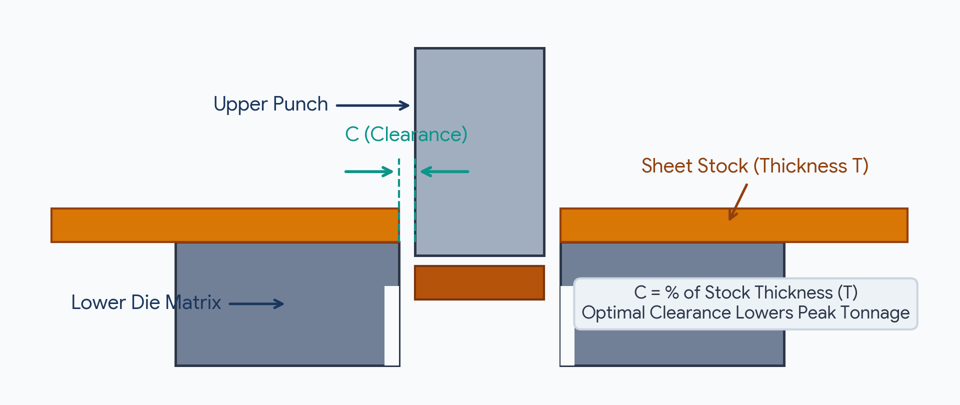
Worn punch edges or improperly matched die clearances multiply the force needed to fracture the metal, pushing the drive motor into higher current draw. Maintaining a disciplined regrinding schedule and selecting optimal clearance ratios can lower peak electrical amperage by up to 15% while extending tool life.
Ram Stroke Travel and Bottom-Dead-Center Dwell
Over-stroking the ram wastes electrical energy on unnecessary vertical travel. Programming the upper reversal point just high enough to clear the sheet surface—and trimming excess dwell time at bottom dead center—simultaneously boosts hit rates and conserves power.
3. Shop-Floor Operating Habits to Trim Kilowatt-Hours
Shifting Heavy-Tonnage Runs to Off-Peak Utility Windows
Commercial electricity tariffs frequently drop substantially during overnight hours and weekends. Scheduling thick-plate punching or extended batch runs during off-peak billing tiers can trim monthly facility electricity expenses by roughly 15% to 20%.
Streamlining Nesting and Tool-Path Sequences
Sequencing hits by geometric proximity prevents servo axes from repeatedly accelerating and decelerating across the worktable. Enabling energy-conscious nesting modes inside your CAM software and tuning acceleration ramps to match press dynamics keeps axis power spikes to a minimum.
Activating Standby and Automated Sleep Functions
Modern CNC punching centers incorporate eco-standby modes that de-energize hydraulic pumps and servo drives during idle pauses. Even brief 30-second loading delays accumulate into substantial wasted energy across thousands of shifts, making operator discipline around standby activation vital.
4. Preventive Maintenance and Hardware Retrofits for Long-Term Savings
Deploying Condition-Based Predictive Maintenance
Continuous monitoring of hydraulic fluid temperature, motor phase current, and frame vibration exposes mechanical drag or valve leakage long before catastrophic faults drive up power consumption. Logging these baseline metrics weekly lets maintenance teams intervene proactively.
Installing Variable-Frequency Drives (VFDs) on Legacy Presses
For older punch presses driven by constant-speed induction motors, retrofitting a VFD offers one of the fastest capital returns—commonly achieving payback in under 24 months on machines experiencing fluctuating duty cycles.
Upgrading to Direct-Drive Servo-Electric Punching Systems
All-electric servo punching presses completely remove hydraulic oil circuits, eliminating both continuous pump losses and chiller cooling loads. Replacing an aging hydraulic press with a modern servo-electric system routinely delivers 30% to 40% energy reductions while cutting annual maintenance costs in half.
5. Frequently Asked Questions (FAQs)
Q1: How can a fabrication shop accurately measure punching machine power consumption?
Install a dedicated inline sub-meter or clamp-on power logger on the press's main electrical feeder to record kWh per shift and per part batch. Comparing energy logs across different alloys and thicknesses quickly highlights inefficient setups.
Q2: How much does compressed air contribute to a punch press's total energy footprint?
Pneumatic circuits used for slug evacuation, tool lubrication misting, and part blow-off typically account for 5% to 10% of total machine energy use. Repairing manifold leaks and regulating air pressure to the lowest effective PSI prevents continuous compressor waste.
Q3: Do energy-efficient punching machines justify their higher initial purchase price?
For medium-to-high-volume fabricators, the answer is a clear yes. When industrial electricity rates exceed $0.10 per kWh, lower utility bills and reduced hydraulic maintenance typically recover the upfront price difference within 18 to 36 months.
6. Conclusion & Partnering with JUGAO Lowering the electrical footprint of sheet metal punching requires a balanced combination of high-efficiency drive hardware, intelligent CAM programming, and disciplined tooling maintenance. By modernizing motors and drives, refining hit sequences, and keeping cutting edges sharp, your facility can substantially reduce kilowatt-hour expenses without sacrificing throughput or edge quality. Ready to benchmark your current press line or explore next-generation servo-electric solutions? Contact the JUGAO engineering team today—we will help you identify immediate energy-saving wins and high-ROI upgrades tailored to your production goals. |
Related
Keep
reading.
 What equipment is best for welding stainless steel? Are there risks of weak welds or deformation?
 CNC Turret Punch Presses Explained: Architecture and Operation
 Key Factors Governing Optimal Punch Press Tonnage
 Comparison of Laser Welding Results and Application Scenarios Across Different Materials
 How to Choose Between Air-Cooled and Water-Cooled Laser Welding Systems
 Understanding Punching Machines: Principles, Types, and Selection
 How can one effectively follow the installation guidelines for a pipe-bending machine?
 For which types of products is an automatic wire-feeding laser welding machine suitable?
 What Are the Latest Punching Machine Trends and Technological Breakthroughs?
 What Triggers Punching Machine Noise and How Can You Quieten It?
 What factors influence the replacement cycle of wear parts in a pipe-bending machine?
 Beyond price, what key parameters should you consider when purchasing welding equipment?
Engineering review
Send a drawing.
Get an engineer.
Standard selections answered within 4 hours. Parts outside the rules get a written process review within 24 hours.
- Part drawing: DXF, DWG, STEP or PDF
- Material and thickness
- Longest bend or cut length
- Yearly volume
Write to info@ntjugao.com or message the factory on WhatsApp +86 132 2211 1178.
Drawings (DXF, DWG, STEP, PDF): attach them to an email to info@ntjugao.com, quoting your name.