 Get a quote
Resources
What is the difference between spot welding machines and laser welding machines?
In metal processing and manufacturing, both spot welding machines and laser welding machines are common types of welding equipment; however, they differ significantly in terms of welding principles, suitable applications, equipment structure, and production methods.
For businesses seeking welding equipment manufacturers, the first step when faced with various options on the market is to understand the differences between spot welding and laser welding. Equipment should be selected based on specific product characteristics and production requirements, rather than simply trying to determine which type is "better."
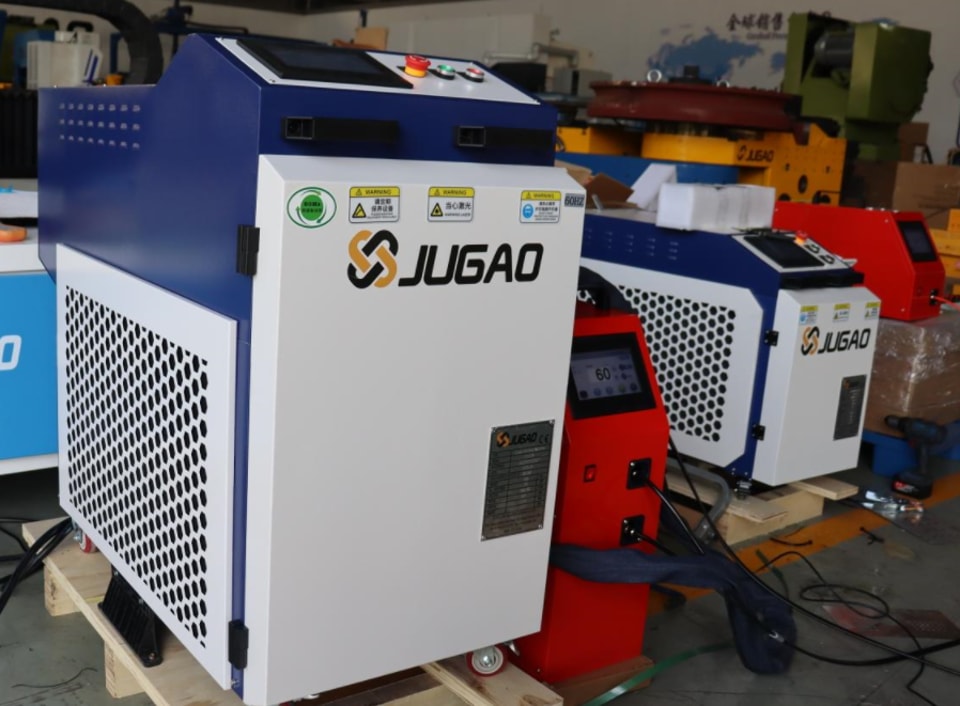
So, what exactly distinguishes spot welding machines from laser welding machines, and for which scenarios is each best suited?
I. Different welding principles
Spot welding machines are a type of resistance welding equipment. They primarily function by applying pressure to the workpiece via electrodes while simultaneously passing a welding current through it; this generates heat at the contact area, creating a weld spot.
Consequently, spot welding typically requires physical contact between the electrodes and the workpiece. It is well-suited for products that require connections at specific, fixed points.
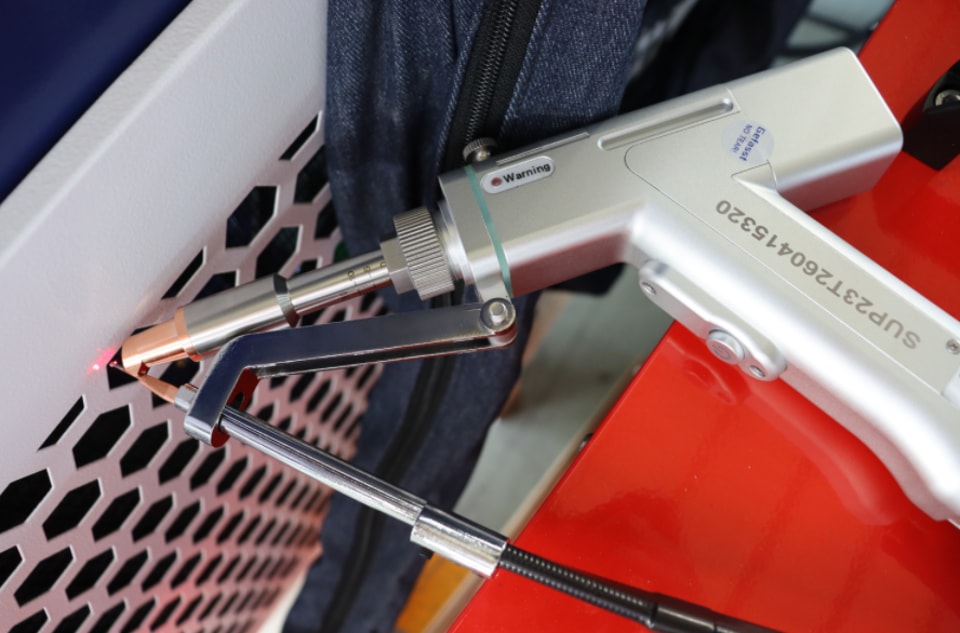
Laser welding machines, on the other hand, utilize a high-energy-density laser beam directed at the material's surface, causing the weld zone to melt rapidly and form a weld seam. Depending on the product structure, laser welding can be performed as continuous welding, spot welding, or welding along a specific path.
Simply put:
Spot welding focuses on "joining via weld spots," whereas laser welding focuses on "joining via laser-induced melting."
There is no simple one-to-one replacement relationship between the two; the actual choice depends on the product structure and process requirements.
II. Which products are best suited for spot welding machines?
Spot welding is characterized by high welding speeds and suitability for multi-point connections, making it widely used in mass manufacturing.
Examples include:
Metal wire products and mesh panels;
Hardware stampings;
Sheet metal structural components;
Metal parts for home appliances;
Automotive components;
Metal connectors for electronics and electrical appliances;
Metal components for batteries and new energy applications.
For certain products, the workpiece is designed with multiple fixed weld points; the process simply requires accurately positioning the upper and lower layers of material and using electrodes to complete the weld. In such cases, spot welding equipment is often the more straightforward choice.
III. Which products are best suited for laser welding machines?
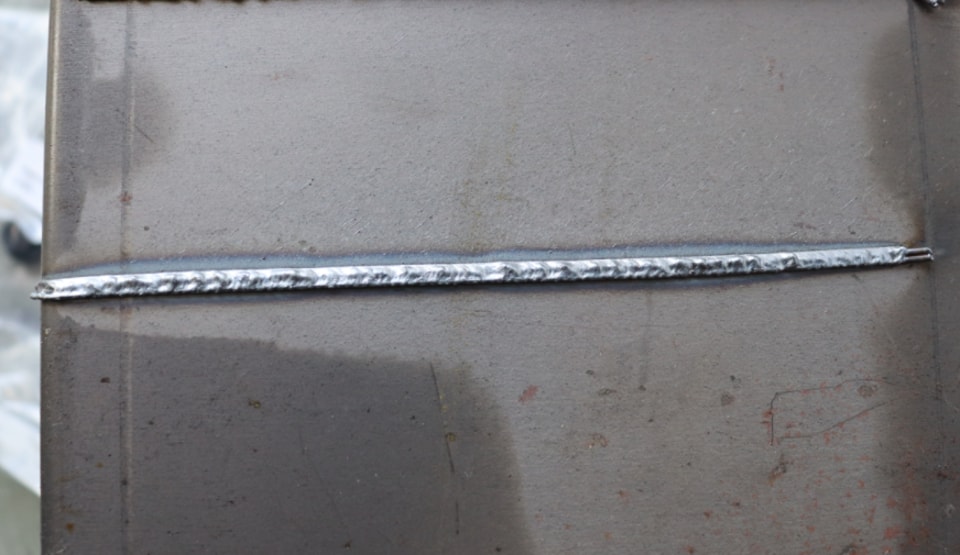
One characteristic of laser welding is the concentration of the weld zone; the welding path can be tailored to the product's structural design. Consequently, it is widely used in precision metal processing, applications requiring high aesthetic standards, and the production of complex structural components.
Common applications include:
Hardware and sheet metal: Welding of metal structural parts such as stainless steel and galvanized sheets;
New energy and energy storage: Battery enclosures, metal structural components, etc.;
Home appliances and kitchenware: Metal housings, brackets, and related structural parts;
Precision electronics manufacturing: Metal parts requiring high welding precision and aesthetic quality;
Automotive and components: Welding of specific metal structural parts and components.
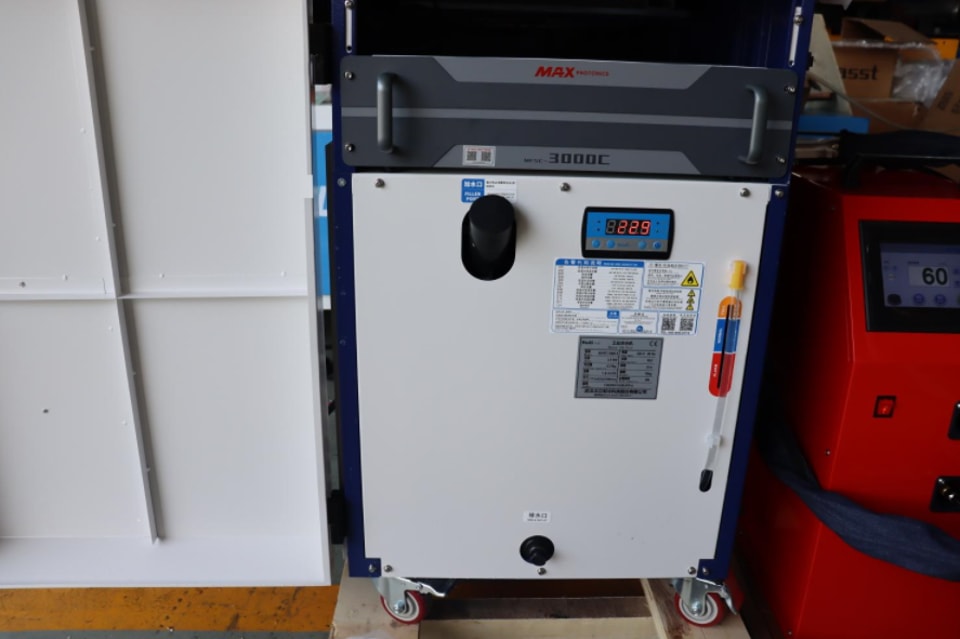
Laser welding equipment comes in various forms, such as handheld laser welders with automatic wire feeders, air-cooled laser welders, flatbed "mark-free" laser welders, galvanometer-based laser welders, and robotic laser welding workstations.
Therefore, "laser welder" does not refer to a single type of equipment; the specific choice depends on the product's manufacturing process requirements.
IV. How do the production methods of spot welding and laser welding differ?
There are significant differences in production methods between the two welding processes.
Spot welding typically requires the electrode to make contact with the workpiece; the welding location is constrained by the electrode's structure and the accessibility of the workpiece. For products requiring numerous weld points, production efficiency can be improved through multi-point welding, specialized tooling, or automated equipment.
Laser welding, by contrast, directs the beam onto a specific location. It can weld areas that are difficult for traditional electrodes to reach by utilizing the equipment's configuration and appropriate tooling.
In automated production, laser welding can be integrated with robots, motion platforms, and vision positioning systems to achieve highly flexible control over the welding path.
Therefore, spot welding is a strong candidate for products requiring fixed weld points and high-speed, batch-style joining. Laser welding should be considered for products requiring continuous seams, complex paths, or high aesthetic standards for the weld.
V. How do you choose between a spot welder and a laser welder?
When purchasing equipment, enterprises can evaluate options based on the following factors:
Comparison Criteria | Spot welding machine | Laser welding machine |
Welding Method | Resistance welding | Laser fusion welding |
Primary Joint Configuration | Spot welding | Spot welding, continuous seam welding, path welding |
Workpiece Contact | Typically requires electrode contact | Laser beam applied to the welding zone |
Common Applications | Stamped parts, wire mesh, hardware components, etc. | Sheet metal, precision parts, structural components, etc. |
Automation Type | Multi-point welding, automatic spot welding | Platforms, galvanometer scanners, robots, etc. |
Key Selection Factors | Current, pressure, time, electrodes, etc. | Laser power, material, sheet thickness, weld seam, etc. |
Note: This table serves only for a preliminary understanding and should not be used as the sole basis for equipment selection.
Before finalizing the equipment choice, it is essential to conduct process validation using actual product samples.
VI. Why is trial welding recommended when purchasing welding equipment?
Whether choosing spot welding or laser welding, relying solely on product names or equipment specifications can lead to inaccuracies.
For instance, even with stainless steel products, variations in plate thickness, structural design, and weld point locations can result in different requirements for equipment configuration and welding parameters.
A logical workflow is as follows:
Product samples/drawings → Material and thickness confirmation → Weld location analysis → Process plan → Sample trial welding → Inspection of weld quality → Equipment finalization
For enterprises, trial welding not only allows for the assessment of weld quality but also provides early insight into equipment operation, production cycle times, and the compatibility between the product and the equipment.
Conclusion
Spot welding is better suited for products primarily requiring fixed-point connections, whereas laser welding accommodates continuous seams, path welding, and applications demanding high precision and superior aesthetic finishes. When selecting welding equipment, the most critical factor for enterprises to consider is the compatibility between the product and the welding process.
Related
Keep
reading.
 Comparison of Laser Welding Results and Application Scenarios Across Different Materials
 How to Choose Between Air-Cooled and Water-Cooled Laser Welding Systems
 Understanding Punching Machines: Principles, Types, and Selection
 How can one effectively follow the installation guidelines for a pipe-bending machine?
 For which types of products is an automatic wire-feeding laser welding machine suitable?
 What Are the Latest Punching Machine Trends and Technological Breakthroughs?
 What Triggers Punching Machine Noise and How Can You Quieten It?
 What factors influence the replacement cycle of wear parts in a pipe-bending machine?
 Beyond price, what key parameters should you consider when purchasing welding equipment?
 4 Common Methods for Inspecting Weld Quality
 Selecting the Top Punching Machines for Small Workshops & Heavy Industry
 How do you set the welding path for a robotic laser welding machine? Can it perform precise welding on complex workpieces?
Engineering review
Send a drawing.
Get an engineer.
Standard selections answered within 4 hours. Parts outside the rules get a written process review within 24 hours.
- Part drawing: DXF, DWG, STEP or PDF
- Material and thickness
- Longest bend or cut length
- Yearly volume
Write to info@ntjugao.com or message the factory on WhatsApp +86 132 2211 1178.
Drawings (DXF, DWG, STEP, PDF): attach them to an email to info@ntjugao.com, quoting your name.