 Get a quote
Resources
What causes bending defects due to temperature issues in pipe bending machines?
The issue of temperature in pipe bending machines is actually quite subtle. Your program and mold may be fine, but the bent pipes just won't turn out right—the first batch is good, the second batch is off-center; pipes dried in the morning pass inspection, but those dried in the afternoon are all off-center. Often, it's not the machine that's broken, but the temperature that's quietly at play.
I. Metal Expansion When Heated
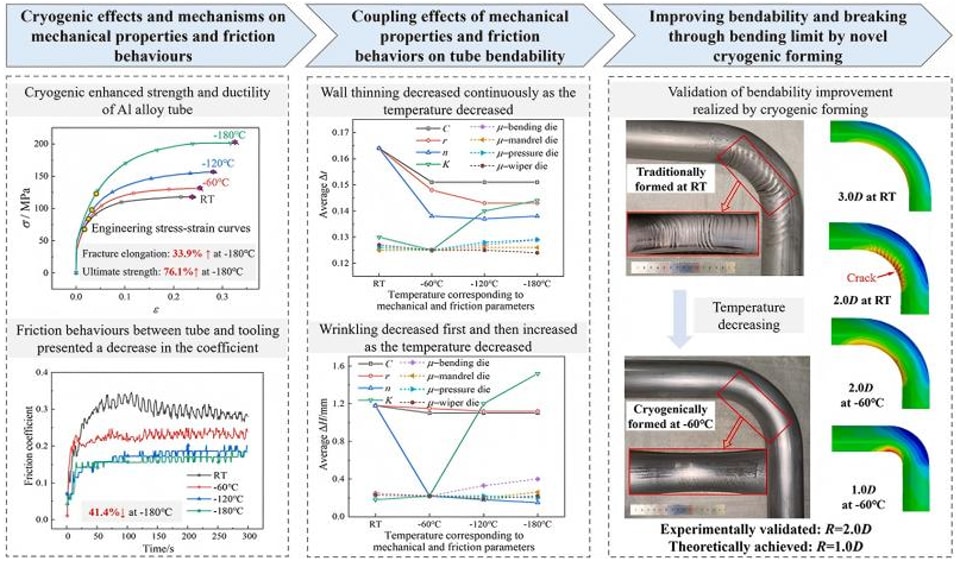
During pipe bending, the pipe itself gradually heats up due to deformation and friction. Higher temperatures cause the metal to expand, resulting in slight changes in wall thickness distribution, diameter, and even length. For steel, this change might be subtle, but for aluminum, the effect of thermal expansion is more significant.
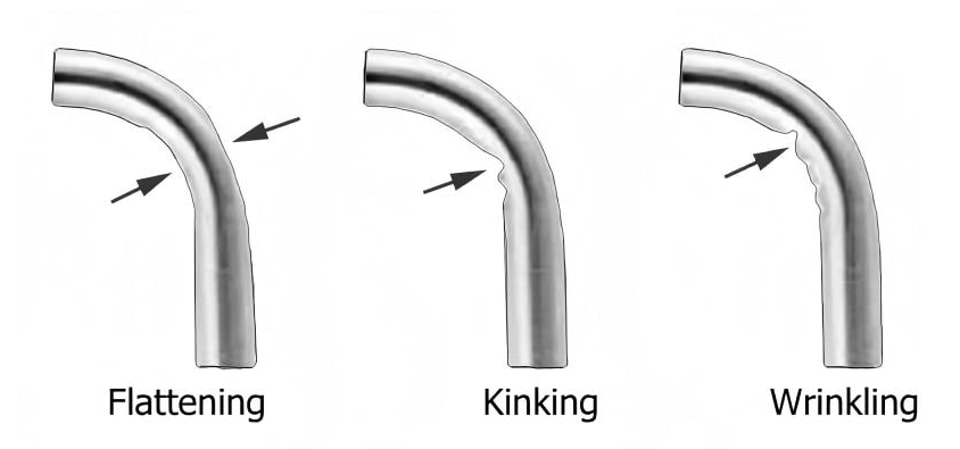
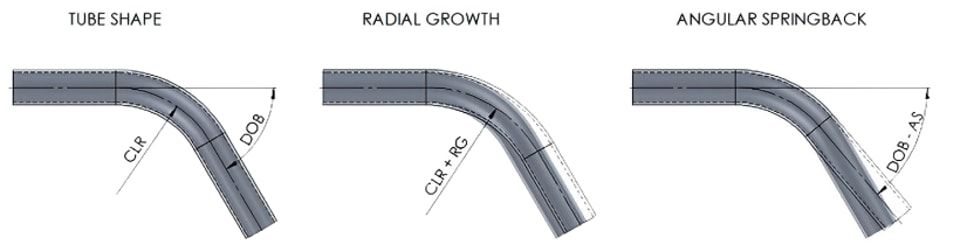
More troublesome is that the springback characteristics of materials differ between hot and cold states. The same program might produce a perfectly bent angle with a cold pipe, but with a hot pipe, the springback might be less or more. This is why the quality of pipes made by the same machine at different times varies—the ambient temperature changes, and so does the material temperature.
II. Mold Temperature Also Changes
During the pipe bending process, there is constant friction between the pipe and the mold. After bending a certain number of times, the temperatures of the bending die, clamping die, and mandrel will gradually rise. Higher die temperatures alter the contact state between the pipe and the die.
Potential problems at this point include: scratches on the pipe surface, uneven bending resistance, and failure of the bending oil on the contact surface. These problems don't appear immediately; they often manifest gradually after a period of operation. Operators typically don't connect these problems to the die temperature.
III. Hydraulic Oil Temperature Directly Affects Bending Force
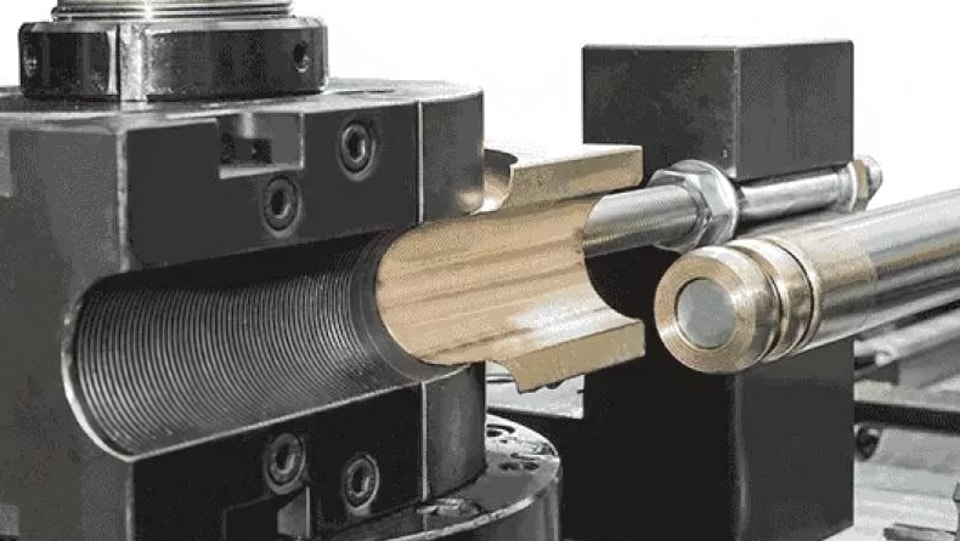
Hydraulic oil is the force transmission medium in a hydraulic pipe bending machine. Changes in oil temperature alter its viscosity, affecting the system's pressure transmission efficiency.
At low temperatures, the oil is thick, resulting in a slower system response and potentially less crisp clamping and bending actions. At high temperatures, the oil is thin, increasing internal leakage and making it difficult to maintain pressure, potentially leading to insufficient bending force. The result is a bending angle that is either too large or too small.
During prolonged continuous production, the oil temperature will continue to rise. If left uncontrolled, the oil temperature may exceed the acceptable range, affecting not only accuracy but also accelerating the aging of seals.
IV. Seasonal Impact of Ambient Temperature
The low workshop temperature in winter and the high temperature in summer also affect the pipe bending machine.
When starting the machine cold in winter, the clearances between machine components are smaller due to the low temperature, and the hydraulic oil is also thicker. If batch production is started directly without preheating, the quality of the first few pipes may differ from later ones.
Some experienced operators have developed a habit of running the machine idle for ten minutes after startup to allow the machine temperature to stabilize before starting work. This practice is quite reasonable.
V. Several Methods for Temperature Control
After starting the machine each day, run it idle for a period of time to allow the hydraulic oil temperature to rise and all components to reach thermal equilibrium before starting formal production.
During continuous large-scale production, carefully observe the oil temperature gauge. If the oil temperature remains consistently high, check if the cooling system is working properly, if the cooling fan is running, and if the oil cooler is blocked.
The choice of pipe bending oil is also very important. Different brands of pipe bending oil have different applicable temperature ranges. Choosing an oil suitable for your production environment will result in more stable lubrication.
For high-precision production, consider installing air conditioning or ventilation equipment in the workshop to reduce the impact of ambient temperature fluctuations on the machines.
VI. Some Methods for Daily Observation
An oil temperature gauge is an important reference for judging whether the cooling system is working properly. Also, pay attention to the changes in the contact temperature of moving parts during machine operation. Differences that operators perceive daily can also be used as a reference factor.
If you find a significant correlation between the quality of the bent pipes and changes in time and temperature, it can be basically determined that temperature is affecting the accuracy. Record the ambient temperature, oil temperature, machine running time, and bent pipe quality data, and compare them to see the pattern.
Have you encountered cases in production where quality fluctuations were caused by temperature changes? How did you determine that it was related to temperature? Welcome to share. The issue of temperature in pipe bending machines is actually quite subtle. Your program is fine, the mold is fine, but the bent pipes are just not right—the first batch is good, the second batch is off-center; the ones done in the morning pass inspection, the ones done in the afternoon are all off-center. Many times, it's not that the machine is broken, it's that temperature is at play.
Have you encountered any cases in production where quality fluctuations were caused by temperature changes? How did you determine that it was related to temperature?
Related
Keep
reading.
 Comparison of Laser Welding Results and Application Scenarios Across Different Materials
 How to Choose Between Air-Cooled and Water-Cooled Laser Welding Systems
 Understanding Punching Machines: Principles, Types, and Selection
 How can one effectively follow the installation guidelines for a pipe-bending machine?
 For which types of products is an automatic wire-feeding laser welding machine suitable?
 What Are the Latest Punching Machine Trends and Technological Breakthroughs?
 What Triggers Punching Machine Noise and How Can You Quieten It?
 What factors influence the replacement cycle of wear parts in a pipe-bending machine?
 Beyond price, what key parameters should you consider when purchasing welding equipment?
 4 Common Methods for Inspecting Weld Quality
 Selecting the Top Punching Machines for Small Workshops & Heavy Industry
 How do you set the welding path for a robotic laser welding machine? Can it perform precise welding on complex workpieces?
Engineering review
Send a drawing.
Get an engineer.
Standard selections answered within 4 hours. Parts outside the rules get a written process review within 24 hours.
- Part drawing: DXF, DWG, STEP or PDF
- Material and thickness
- Longest bend or cut length
- Yearly volume
Write to info@ntjugao.com or message the factory on WhatsApp +86 132 2211 1178.
Drawings (DXF, DWG, STEP, PDF): attach them to an email to info@ntjugao.com, quoting your name.