 Get a quote
Resources
How to Address Excessive Weld Pool Temperatures in Welding Robots?
Is your welding robot's weld pool temperature running too high? How can you resolve this? Leveraging their inherent advantages, welding robots have elevated the level of automation across various industries, ensured consistent weld quality, and maximized welding efficiency. Welding robots are capable of operating around the clock. However, as operating times extend, the temperature of the weld pool inevitably rises. Once the weld pool temperature becomes excessively high, it can negatively impact both the welding process and the equipment itself.
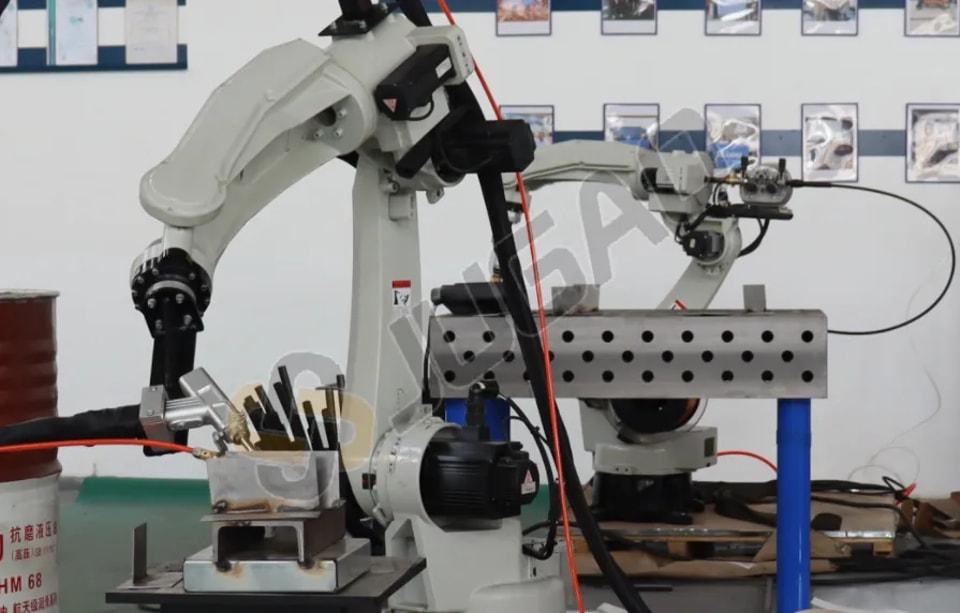
Addressing excessive weld pool temperatures in robotic welding requires careful consideration of several factors, including the electrode angle, arc duration, electrode diameter, and welding technique.
1. Electrode Angle
When the angle between the electrode and the direction of welding falls within a moderate range, the arc becomes concentrated, resulting in a high weld pool temperature; conversely, if the angle is too acute, the arc disperses, leading to a lower weld pool temperature. When selecting the electrode angle, it is essential to base the choice on the specific welding process being employed, as this contributes to stabilizing weld quality.
2. Arc Duration
To regulate the weld pool temperature, an intermittent arc technique (or "arc-breaking" method) may be utilized during welding. Specifically during root pass welding (sealing the bottom of the joint), both the frequency of arc interruption and the duration of the active arc directly influence the weld pool temperature. If the weld pool temperature becomes excessively high—resulting in an overly large melt-through hole—the arc duration can be shortened to lower the temperature. This approach helps maintain a smaller melt-through hole and ensures a moderate bead height on the inside of the pipe, thereby preventing excessive internal weld protrusion or the formation of weld lumps (blobs).
3. Electrode Diameter
Welding Current and Electrode Diameter: The welding current and electrode diameter should be selected based on the spatial position of the weld joint and the welding orientation. At the commencement of welding, a larger welding current and electrode diameter are typically appropriate; however, for vertical or overhead welding positions, a lower current and smaller electrode diameter are generally required. The foundation for achieving a well-formed weld lies in the judicious selection of the welding current and electrode diameter, as this facilitates effective control over the weld pool temperature.
4. Selection of Appropriate Welding Parameters
Welding parameters primarily encompass the welding current, voltage, torch position and orientation, wire feed speed, and similar variables. The welding current and voltage should be adjusted as necessary to ensure optimal weld quality. To prevent the weld pool temperature from escalating due to prolonged operation at high currents, the operator can make appropriate adjustments to the welding parameters based on the quality of the resulting weld bead.
The above points outline how welding robots can be managed to control weld pool temperatures. Maintaining an appropriate weld pool temperature is crucial for preserving weld quality and enhancing the user's overall production efficiency.
Related
Keep
reading.
 Comparison of Laser Welding Results and Application Scenarios Across Different Materials
 How to Choose Between Air-Cooled and Water-Cooled Laser Welding Systems
 Understanding Punching Machines: Principles, Types, and Selection
 How can one effectively follow the installation guidelines for a pipe-bending machine?
 For which types of products is an automatic wire-feeding laser welding machine suitable?
 What Are the Latest Punching Machine Trends and Technological Breakthroughs?
 What Triggers Punching Machine Noise and How Can You Quieten It?
 What factors influence the replacement cycle of wear parts in a pipe-bending machine?
 Beyond price, what key parameters should you consider when purchasing welding equipment?
 4 Common Methods for Inspecting Weld Quality
 Selecting the Top Punching Machines for Small Workshops & Heavy Industry
 How do you set the welding path for a robotic laser welding machine? Can it perform precise welding on complex workpieces?
Engineering review
Send a drawing.
Get an engineer.
Standard selections answered within 4 hours. Parts outside the rules get a written process review within 24 hours.
- Part drawing: DXF, DWG, STEP or PDF
- Material and thickness
- Longest bend or cut length
- Yearly volume
Write to info@ntjugao.com or message the factory on WhatsApp +86 132 2211 1178.
Drawings (DXF, DWG, STEP, PDF): attach them to an email to info@ntjugao.com, quoting your name.