What is the structural composition of the three-roller CNC plate rolling machine and how to roll cones?
2026-10-23
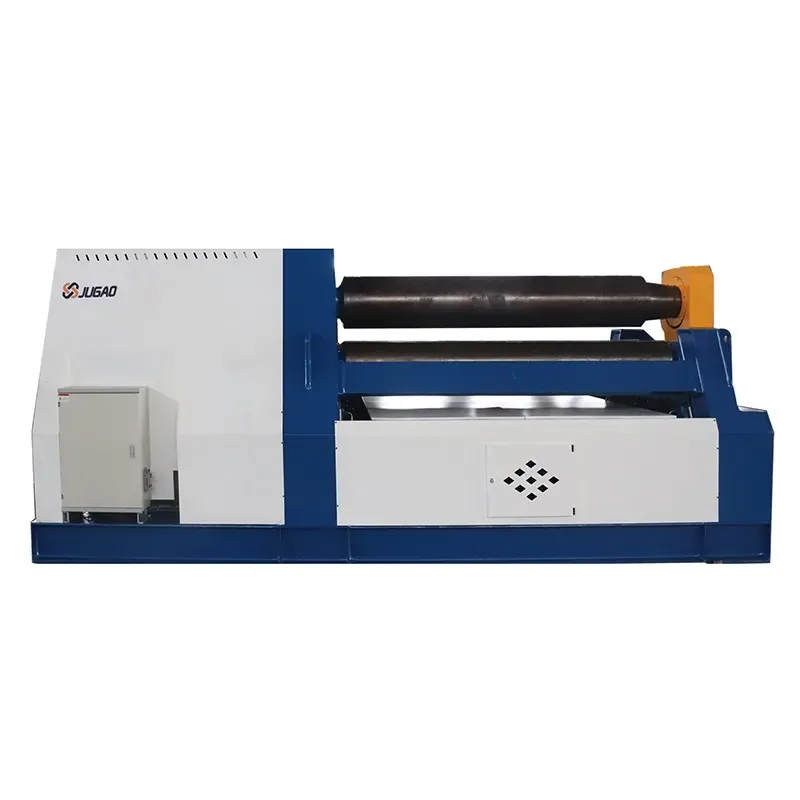
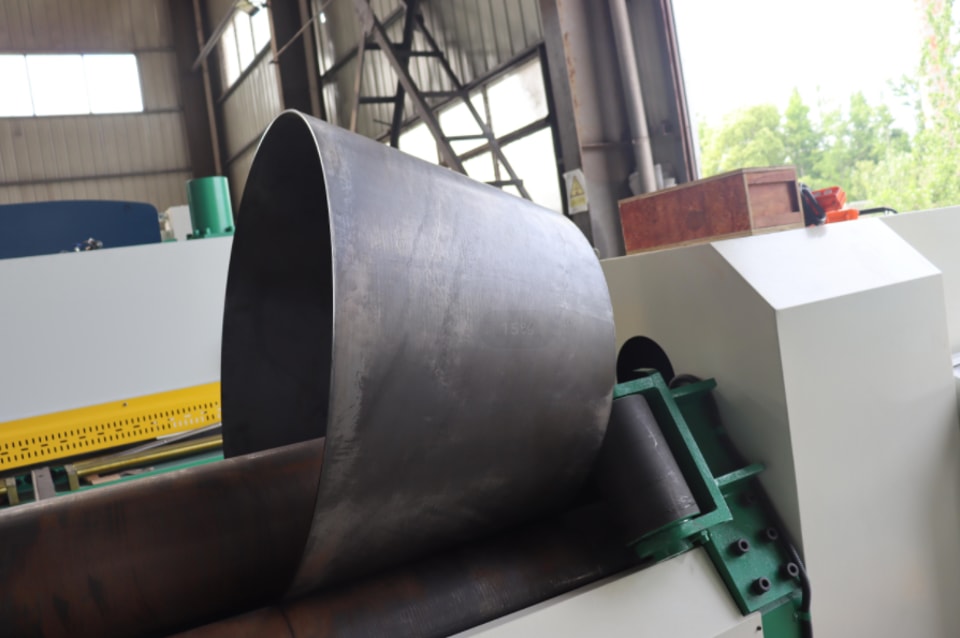
The three-roller plate rolling machine is a shaping machine tool that performs continuous point bending of plates. It can roll metal plates into circular, arc-shaped and tapered workpieces within a certain range.
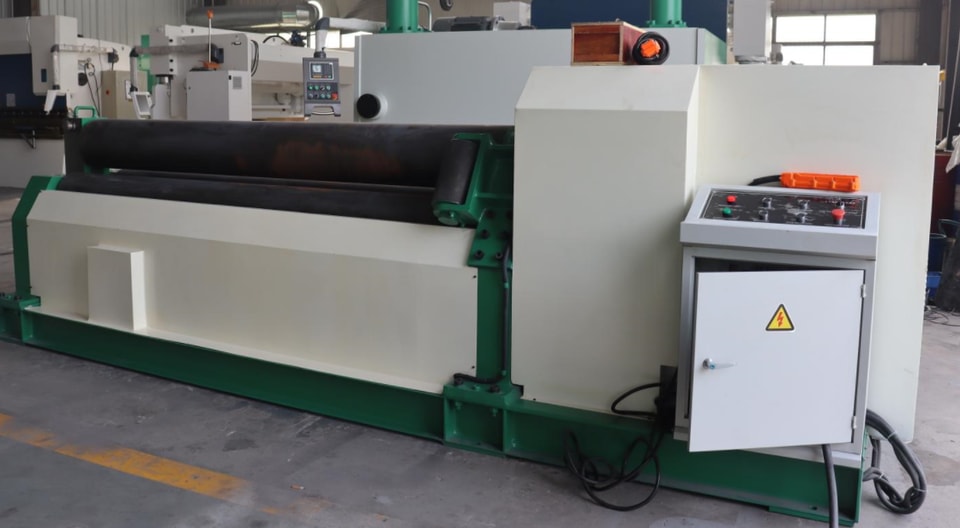
The six major structural components of the three-roller plate rolling machine:
(1) Upper and lower rollers: They are important components of the plate rolling machine, made of forged high-quality carbon steel.
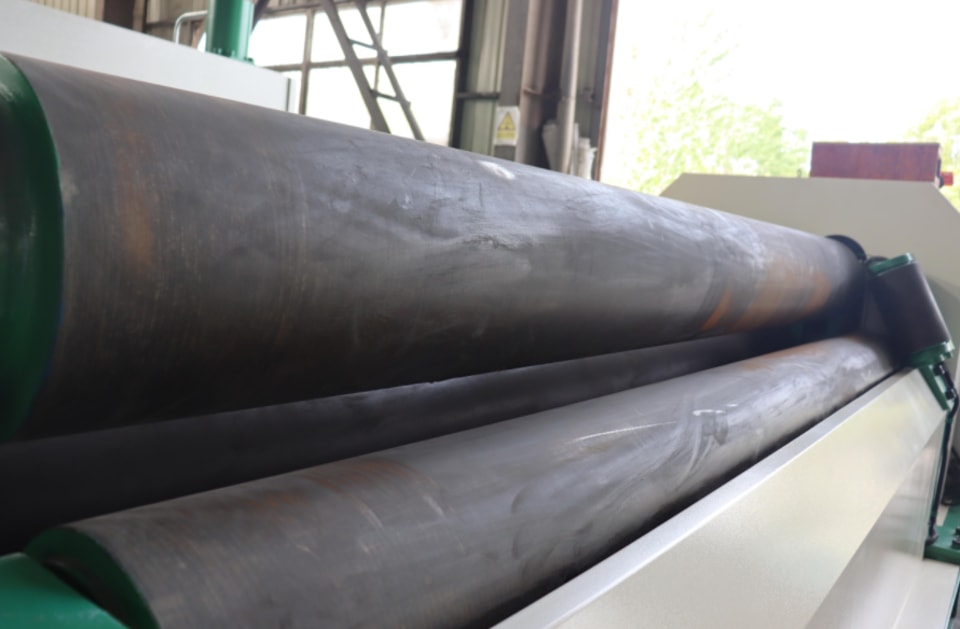
(2) Frame: There are one left and right frame each, and the lower roller bearing is installed on the frame. There is a square buckle screw inside the frame, and the upper end of the screw is hinged with the bearing seats at both ends of the upper roller.
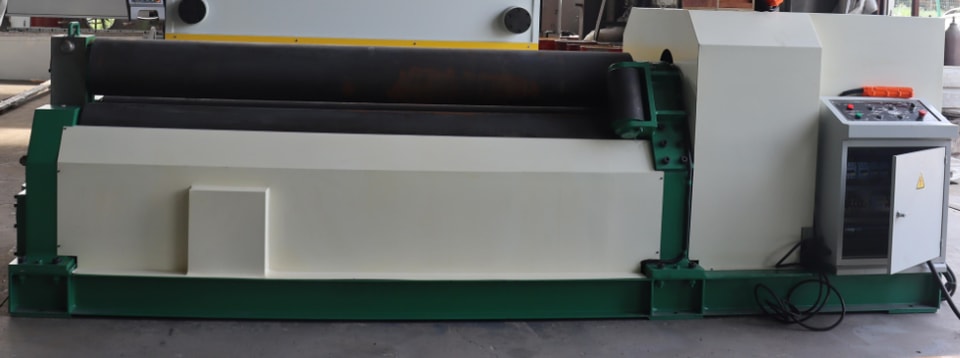
(3) Reducer: ZSY280 hard tooth surface type reducer is installed on the channel steel base together with the pad.
(4) Electrical part: All installed in a control box for easy operation.
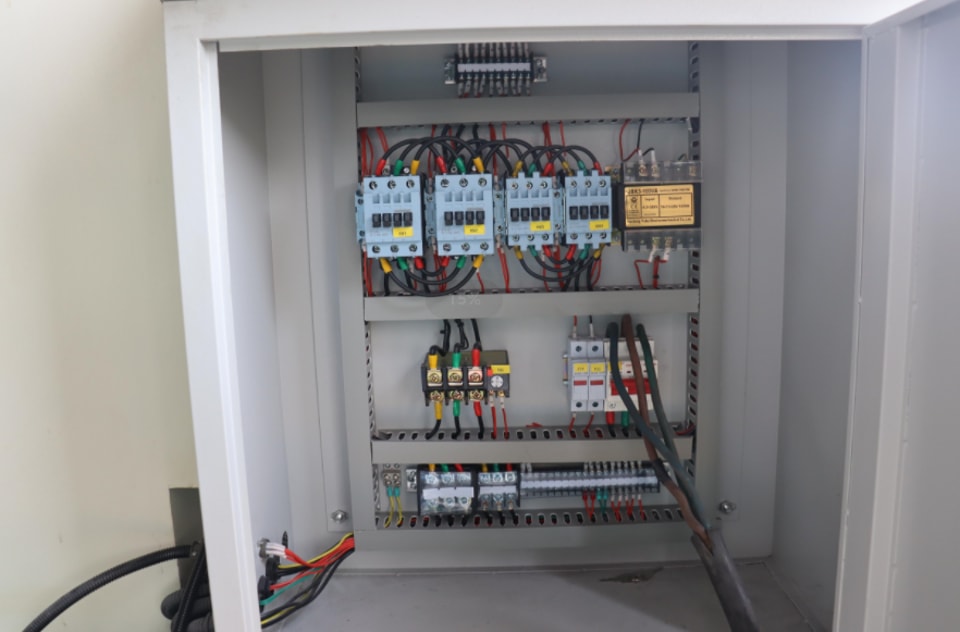
(5) Unloading device: It is installed on the side of the reducer to balance the upper roller when unloading; the unloading and recovery are completed by the oil cylinder.
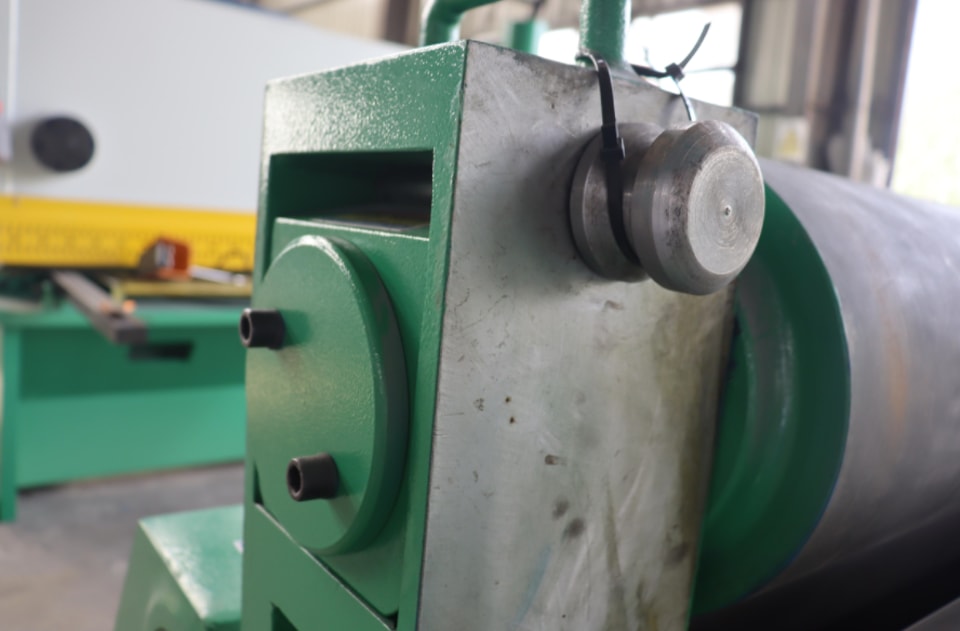
(6) Base: made of welded steel and steel plates. Install the frame, reducer, motor, etc. on it to form a whole.
How to use a three-roller CNC plate bending machine to process cone workpieces?
1. Generally, plate rolling machines can roll cones with a small taper (30 degrees). The key point of rolling cones is that the linear speed of the big and small ends is basically the same. Since the linear speed of the upper roller is the same, the linear speed of the big end must be controlled. It's even easier if you have a cone setting.
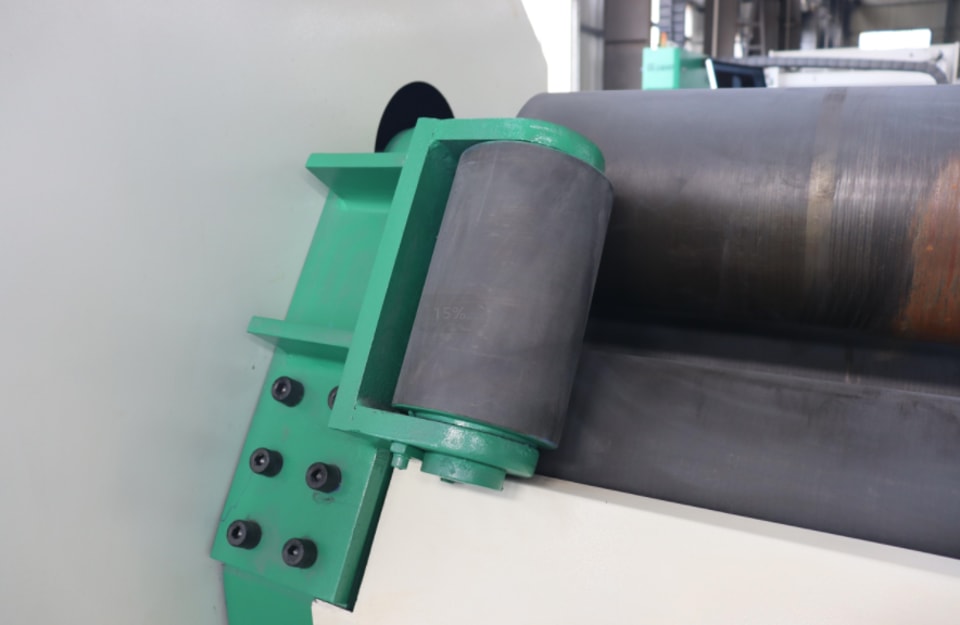
2. Raise one end of the tube on the plate rolling machine, place the small tapered surface at the low end, and keep moving the big end during rolling, and the speed of the big end should be accelerated. Add a side wheel cone device to a section of the roller. There are two cones installed on both sides of the lower roller of the plate rolling machine. When rolling, the small end is pressed against the cone, and the edge of the small end will move in against the cone.
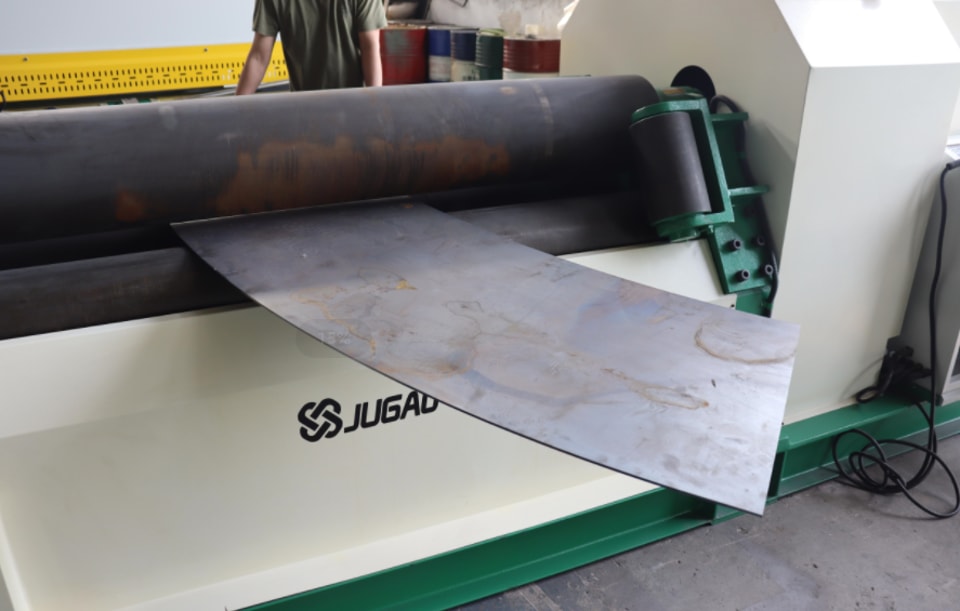
The roller has a certain slope, and the lateral force is very large during rolling. It is necessary to add a lateral deceleration gear wheel, and the gear wheel needs to be quenched. If the diameter is small, the plate is thin, and the roll is long, the three rollers can be made into conical rollers, but the required arc must be calculated well.
3. Adjust the synchronization shaft with a cone device. Before the plate rolling machine is rounded, the straight edge of the cylinder must first be removed. The length of this straight edge varies depending on the model and type of the plate rolling machine. It can be determined by referring to the equipment manual.
Contact Us